

Send Us A Message
Calculating Energy Use and Payback for a Reclaimed Rubber Production Line
Calculating Energy Use and Payback for a Reclaimed Rubber Production Line
For a business evaluating a reclaimed rubber machine, the purchase price is only the visible part of the decision. Electricity demand, steam or thermal energy, labor, maintenance, scrap recovery, and operating uptime will determine whether the line becomes a profitable asset or an expensive bottleneck. This is especially true when production involves waste tire rubber, where feedstock quality and process control can change energy consumption from shift to shift.
A practical payback calculation does not need to be overly complicated. It does, however, need to reflect the way the equipment will actually run in your plant—not merely the rated motor power shown on a quotation. Decision-makers should look at energy per tonne of reclaimed rubber, annual output at realistic utilization, and the value created by replacing virgin rubber or purchasing less reclaimed material from outside suppliers.
Begin with energy per tonne, not nameplate power
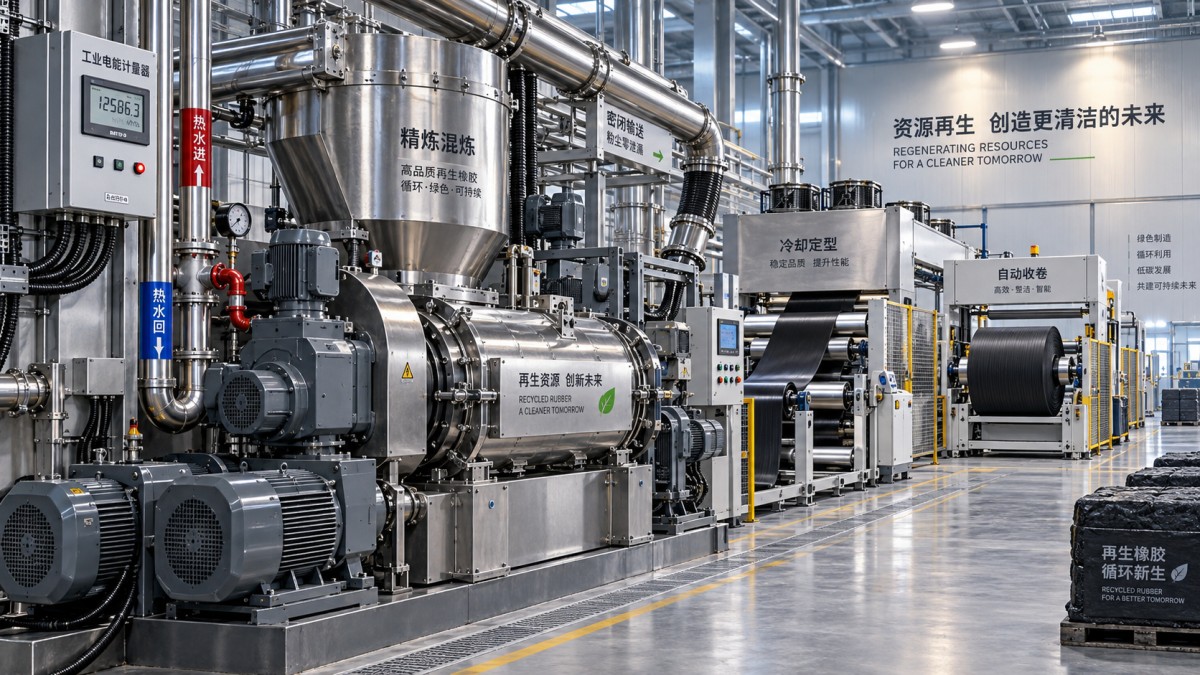
Every reclaimed rubber production line includes multiple energy-consuming sections: material feeding, crushing or refining, mixing, devulcanization or reclaiming, cooling, sheeting, winding, dust collection, conveying, and control systems. A machine may have a high installed power rating but operate at partial load for much of the day. Conversely, an undersized system can draw heavily, stop frequently, and deliver poor output per kilowatt-hour.
The useful starting point is the line’s specific energy consumption:
Specific energy consumption (kWh/t) = Total electricity used (kWh) ÷ Reclaimed rubber output (t)
For example, assume a plant records 18,000 kWh of electricity during a production period and produces 60 tonnes of saleable reclaimed rubber:
18,000 kWh ÷ 60 t = 300 kWh per tonne
This number should be tracked by product grade and feedstock type. Rubber powder from clean industrial scrap behaves differently from tire-derived material containing textile, steel residue, moisture, or inconsistent particle sizes. Comparing only daily electricity bills can hide these differences; comparing kWh per tonne reveals whether the process is improving.
Thermal energy must also be included where applicable. If the reclaiming process uses steam, thermal oil, natural gas, or another heat source, convert the fuel use into a cost per tonne. Electricity may be the easiest number to measure, but it is not necessarily the largest energy expense.
A simple operating-cost model for procurement reviews
Before selecting a new or refurbished reclaimed rubber machine, create a one-page model using conservative assumptions. It should separate fixed costs from costs that rise with production volume.
Suppose Line A requires 300 kWh per tonne and Line B requires 260 kWh per tonne. At an electricity rate of US$0.10 per kWh, the energy difference is US$4 per tonne. That may seem small until annual volume is considered. At 8,000 tonnes per year, the lower-energy line saves approximately US$32,000 annually in electricity alone. If it also produces more consistent material and reduces waste by even a small percentage, the financial difference can become much larger.
Use your own tariff, operating hours, and output target. A reliable supplier should be willing to clarify which motors are included in installed power, whether dust collection and cooling are counted, and what production assumptions support the quoted capacity.
How to calculate annual savings and payback
The payback period estimates how long the additional investment takes to recover through operating savings or added margin. For a reclaimed rubber project, the formula is straightforward:
Simple payback period = Additional investment ÷ Annual net benefit
Annual net benefit can include lower energy cost, lower maintenance expense, labor savings, higher yield, avoided purchases of externally sourced reclaimed rubber, and additional contribution from higher output. It should also subtract new costs, such as financing charges, added operator training, or higher-cost consumables.
Imagine an existing line is replaced or upgraded at an additional capital cost of US$240,000. The new configuration is expected to generate US$55,000 in annual energy savings, US$25,000 through improved material yield, and US$20,000 from reduced maintenance and stoppages. The estimated annual net benefit is US$100,000.
US$240,000 ÷ US$100,000 = 2.4 years
This is a simple payback, not a full financial valuation. Larger investment committees may also apply discounted cash flow, net present value, tax treatment, depreciation, and financing costs. Still, simple payback remains valuable because it makes the operational logic visible: where is the money coming from, and which assumptions are doing the most work?
Do not overlook throughput and utilization
A line rated for a certain hourly output does not automatically achieve that output over a year. Real capacity is affected by shift patterns, planned maintenance, feeding interruptions, changeovers, material preparation, cleaning, and quality holds.
A more realistic annual output calculation is:
Annual saleable output = Rated hourly capacity × Actual running hours × Performance factor × Yield rate
If a supplier quotes 1 tonne per hour, do not immediately multiply that by every scheduled hour in the calendar. Use a performance factor that reflects your operating discipline and raw-material condition. For an early-stage project, conservative assumptions protect the business case from being built on an idealized production scenario.
It is also worth distinguishing between gross output and saleable output. A reclaimed rubber machine should be evaluated on material that meets the customer’s requirements for consistency, contamination level, plasticity, and processability—not simply on kilograms leaving the discharge point.
New versus refurbished equipment: compare lifetime value
Refurbished machinery can be a sound choice when capital budgets are tight, particularly if the equipment has been properly inspected, upgraded, and tested. Yet the comparison should go beyond “new price versus used price.” Ask whether motors, controls, bearings, transmission components, safety systems, and wear surfaces have been assessed. Confirm the availability of drawings, spare parts, commissioning support, and warranty coverage.
JC INDUSTRY established its Used Machinery and Equipment Recycling Center to refurbish, upgrade, and resell equipment while reducing unnecessary replacement and supporting lower-carbon industrial investment. For buyers, the important point is not simply that a machine is pre-owned; it is whether its expected energy use, condition, reliability, and support arrangements are transparent. A 24-month warranty offered on new and used equipment can provide an additional basis for evaluating risk, but site acceptance criteria should still be clearly documented.
Control and tension-management experience also matters across rubber and sheet-processing applications. For example, features such as EPC-controlled unwinding, tension detection, movable process modules, and motor-driven trimming are used in systems such as the Sport flooring laminating line. While this is a different application from reclaimed rubber production, the same engineering discipline—stable material handling, responsive controls, and maintainable mechanical design—can influence yield and energy efficiency throughout a manufacturing plant.
Questions to ask before approving the project
- What is the expected electricity and thermal-energy consumption per tonne for our intended feedstock?
- Which auxiliary systems are included in the consumption estimate?
- What annual utilization rate is assumed in the supplier’s payback calculation?
- How will moisture, contamination, and particle-size variation affect output and energy use?
- What are the main wear parts, their expected replacement intervals, and their cost?
- Can the line’s actual energy consumption be measured by section after commissioning?
- What production and quality criteria define successful acceptance?
The strongest procurement decision is rarely based on the lowest quoted price or the highest stated capacity. It is based on a credible operating model, measured assumptions, and a clear view of risk. When evaluating a reclaimed rubber machine, calculate cost per tonne, test the sensitivity of the payback period, and give equal attention to energy, yield, uptime, and serviceability. That approach supports both financial discipline and the broader goal of recovering more value from rubber resources with less energy wasted.