










Send Us A Message
Choosing a Vacuum Forming Machine by Sheet Material and Gauge Range
Select a vacuum forming machine from the material and finished-part gauge first, then verify that the heating, clamping, vacuum, forming depth, and tooling arrangement can hold that choice across the production range. A machine that forms a thin polystyrene tray cleanly may be unsuitable for a thick ABS enclosure, even when the nominal sheet size is the same. The sheet must reach a uniform forming condition, remain controlled at the frame, and be drawn into the tool before excessive thinning, cooling, or webbing occurs.
Start with the full sheet specification rather than the target part wall thickness alone. Record material family, nominal gauge, gauge tolerance, sheet width and length, surface finish, color, regrind content, and whether the material is supplied with a protective film. Also identify the deepest draw, smallest radii, undercut requirements, cosmetic surfaces, and post-forming operations. These details determine whether a basic vacuum machine is sufficient or whether pressure assist, plug assist, pre-stretch, or a more rigid forming station is required.
Material behavior changes the machine requirement
Thermoplastics do not respond to heat in the same way. A material with a broad forming window is more forgiving of heater variation and cycle interruption. A material with a narrow window demands closer temperature zoning, repeatable sheet indexing, and faster transfer from heater to mold.
Do not treat heater output as a material-neutral rating. The useful question is whether the heater layout can deliver uniform energy through the chosen sheet gauge without overheating the surface. Thin sheet reacts quickly; thick sheet needs enough dwell for heat to penetrate toward the center. If the top surface looks ready while the core remains too cool, the result can be stress whitening, poor corner definition, or a part that springs back after demolding.
Gauge range defines more than heater size
Machines are often described by a broad gauge capability, but the practical production range is narrower when parts have deep draws, large unsupported areas, or demanding cosmetic requirements. Thin-gauge material places emphasis on fast cycling, accurate indexing, web control, and low marking. Heavy-gauge sheet shifts the selection toward structural rigidity, heating depth, clamp force, platen travel, and tool cooling.
For light sheet, assess whether the clamp frame closes evenly along all sides. A small leak or uneven pressure at the frame can pull a thin sheet out of position, creating skewed trim margins. For heavier sheet, examine frame construction and locking force. The sheet resists stretching, and inadequate clamping can cause edge slip that appears as inconsistent draw depth rather than an obvious clamp failure.
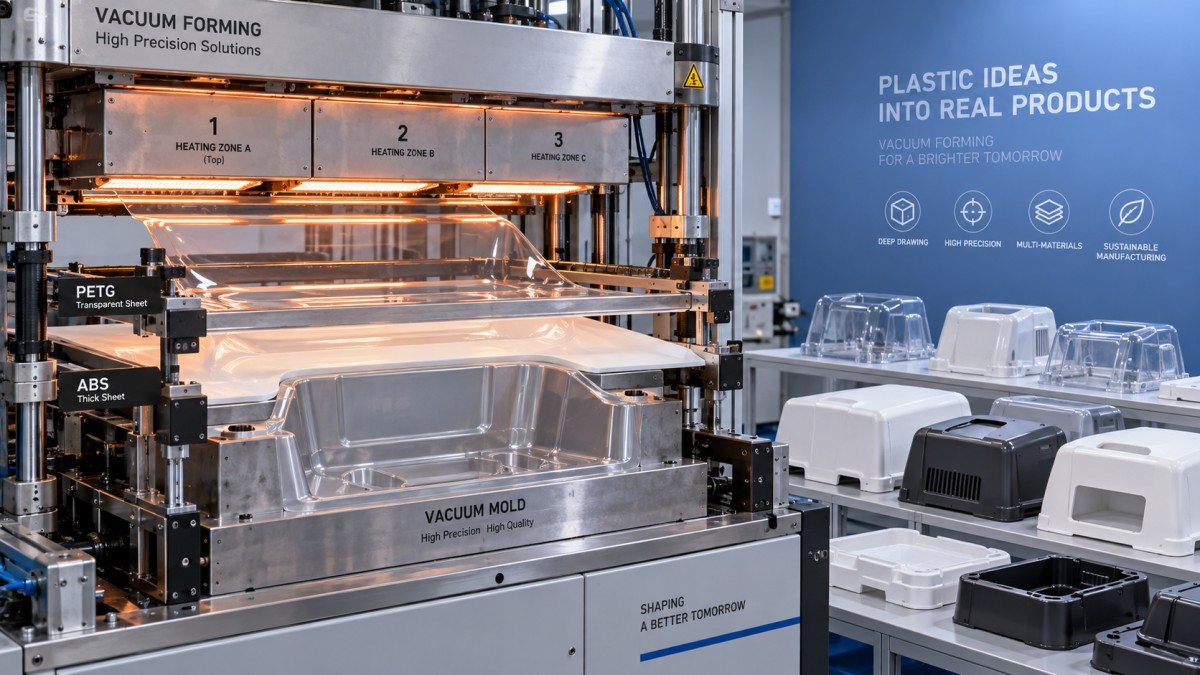
Part geometry magnifies gauge effects. A shallow panel formed from heavy sheet may run well on a machine that cannot produce a tall, narrow housing from the same material. The tall part demands more surface area to be drawn from the original sheet. That extra draw reduces wall thickness unless the process uses pre-stretch, a plug, pressure assist, or a revised part design. A nominal gauge should therefore be evaluated against the thinnest allowable area after forming, especially around corners, ribs, and transition zones.
Match the forming method to the draw problem
Vacuum-only forming is effective for many shallow and moderate-depth components. It becomes less reliable when the tool has sharp detail, a high draw ratio, or large differences between broad flat surfaces and narrow deep features. Vacuum removes air from the mold side of the sheet, but it does not automatically distribute material where it is needed.
- Plug assist mechanically guides hot sheet into a cavity before vacuum completes the draw. It is useful where bottom thickness or corner thickness must be retained. Plug material, finish, temperature, and speed influence the result; a plug that is too cold can mark or chill the sheet, while one that is too hot can drag material unevenly.
- Pressure forming applies positive air pressure above the sheet in addition to vacuum below it. This increases definition and can improve reproduction of texture or fine detail, provided the tool, seals, and machine structure are designed for the higher load.
- Pre-stretch creates a controlled bubble before the sheet contacts the mold. It is particularly relevant for large, deep parts because it reduces the tendency for material to rush from one area of the frame.
Tooling must be considered alongside the machine. Aluminum tools heat and cool differently from resin or composite tools, while vent-hole placement determines whether trapped air prevents complete detail reproduction. A machine with strong vacuum performance cannot compensate for blocked vents, insufficient draft, or a tool that traps the formed part. Confirm platen dimensions, mounting pattern, maximum tool height, and access for cooling lines before releasing the tool design.
Heating control should be evaluated at the sheet, not only at the panel
Separate heater zones are valuable when sheet edges cool faster than the center, when a printed or protected surface needs gentler exposure, or when the part geometry requires more draw in one region. The control system should support repeatable recipes for material and gauge combinations, but recorded setpoints alone do not prove uniform sheet temperature. Commissioning trials should inspect the actual formed wall distribution, corner definition, surface gloss, and trim stability.
Common defects can point to different causes. A thin corner may result from inadequate plug timing, excessive local heating, poor pre-stretch, or a geometry that exceeds the available material distribution. Webbing between adjacent features can be caused by sheet temperature, mold spacing, insufficient draft, or air being drawn into competing cavities too quickly. Treating every defect as a heater problem often leads to repeated adjustments without resolving the underlying restriction.
Specify the production envelope, not a single sample part
A useful specification states the minimum and maximum sheet gauges, the materials expected in normal production, the largest blank, expected tool weights, maximum draw depth, and required forming method. It should also state whether the machine must accommodate protective film, automatic loading, sheet feeding, trimming coordination, or material changeovers. The widest claimed sheet capacity is irrelevant if the clamp opening, heater coverage, or usable mold area does not support the planned tool and trim allowance.
For applications near the upper gauge limit, request trials with production-grade sheet and a representative tool geometry. Evaluate thickness at defined locations after forming, not simply whether the part releases from the mold. Inspect repeatability over several cycles, because initial parts can conceal heat soak, cooling, and sheet-handling variation that appears after the machine reaches normal operating conditions.
Keep adjacent thermal-process equipment separate in scope. A PLC-controlled curing system such as the used_second hand Tyre retreading line uses steam and bladder-based heating for tyre retreading, which is fundamentally different from sheet heating and vacuum draw control. Similar words such as heating, molds, and automatic temperature control do not establish equivalent process capability.
Finally, allow for maintenance access around heaters, vacuum lines, clamps, and mold-change points. Leaking seals, contaminated heater surfaces, blocked vents, and worn frame components can gradually change forming results. A machine selected with adequate thermal capacity, structural margin, and tooling clearance is easier to keep within the intended material and gauge window after installation.