










Send Us A Message
How Reclaimed Rubber Machines Reduce Odor and Batch Quality Variation
For quality-control and safety teams, odor and batch inconsistency are not minor housekeeping issues. A sharp or changing odor can indicate that temperature, residence time, feedstock condition, or ventilation is drifting away from the intended process window. At the same time, variation in reclaimed rubber hardness, dispersion, plasticity, or moisture can create downstream problems in mixing, extrusion, calendaring, and curing.
A well-configured reclaimed rubber machine does not “remove smell” by itself. What it can do is make the conditions that generate odor more controllable: steadier feeding, more consistent heating, better devulcanization control, enclosed transfer points, and clearer process records. That same discipline is what reduces lot-to-lot quality variation.
Why Odor Often Appears Alongside Batch Variation
In reclaimed rubber production, odor is usually linked to volatile compounds released from scrap rubber, residual oils, additives, moisture, or overheating. The exact source depends on the incoming material and the process route. A batch containing different tire fractions, contaminated rubber, excess textile residue, or poorly separated material may behave very differently from the previous one, even when the operator uses the same nominal settings.
The common mistake is to treat odor only as an exhaust-system problem. Strong ventilation is necessary, but it cannot correct unstable thermal history. If a material spends too long in a high-temperature zone, or if one section of the machine runs hotter than another, the plant may see both a stronger odor and a shift in reclaimed rubber properties. The finished material can become overly soft, unevenly treated, or difficult to blend into a downstream compound.
For a QC team, that makes odor a useful early-warning signal. It should not replace laboratory testing, but a sudden change in odor profile deserves attention before the batch reaches the next process. In practice, the most useful investigation starts with material traceability, temperature records, residence time, and the condition of sealing and extraction points.
Stable Feeding Is More Important Than It Looks
The machine can only process what it receives. When feedstock is inconsistent in particle size, moisture, metal contamination, or rubber composition, operators tend to compensate by changing heat or mechanical intensity. That may solve an immediate throughput issue but often creates a less predictable reclaimed rubber output.
A reliable reclaimed rubber machine should support controlled feeding rather than intermittent surges. Consistent feed rates help maintain a stable load in mixing and devulcanization sections. This matters because a machine that is alternately starved and overloaded will not deliver the same shear and heat history to every portion of material. The result can be visible variation in texture, uneven dispersion, and different odor levels across the same production shift.
Before blaming the main processing unit, inspect the upstream steps. Magnetic separation, fiber removal, granulation, storage practices, and moisture control frequently determine whether the equipment can run steadily. A good operating team records feedstock changes by lot rather than relying on broad labels such as “tire rubber” or “mixed scrap.” Those labels are rarely detailed enough for meaningful quality control.
Temperature Control Reduces Both Overprocessing and Odor Peaks
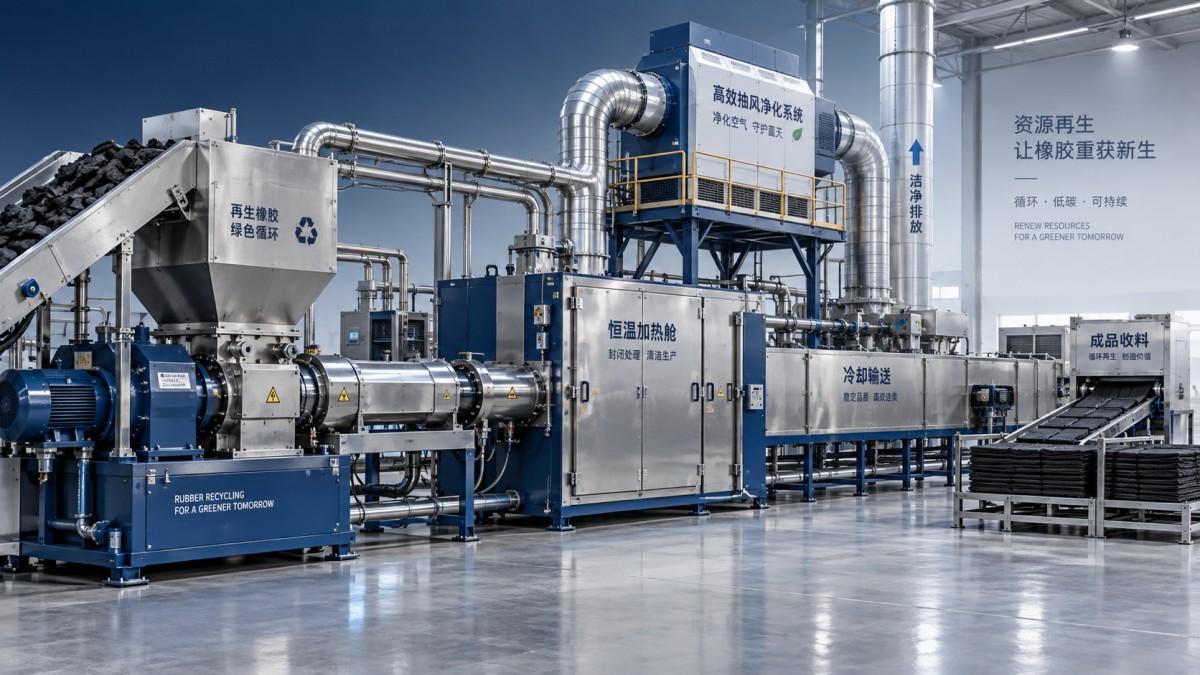
Heat is essential in most reclaimed rubber processes, yet it is also where many quality problems begin. If the material does not receive sufficient thermal and mechanical treatment, devulcanization may be incomplete. If it is exposed to excessive heat or held too long, volatile emissions can increase and polymer degradation may become more likely.
The important point is not simply setting a target temperature. QC personnel should verify whether the actual process temperature is stable across relevant zones and whether the recorded value reflects the material condition rather than only a heater setting. Pressure, fill level, cooling performance, and equipment cleanliness can all affect real heat transfer.
Modern control systems can help by linking feeder speed, motor load, temperature, and processing time. When these values are monitored together, an operator is less likely to correct one abnormal condition by making an aggressive adjustment somewhere else. For example, raising temperature to compensate for poor feed preparation may improve short-term flow but increase odor and introduce a new consistency problem.
Containment and Extraction Must Follow the Material Path
Odor control is strongest when the process is enclosed where emissions are generated. Open transfer points, worn seals, poorly fitted covers, and delayed removal of warm processed material can allow odor to spread into work areas before extraction can capture it. This becomes a safety-management concern as well as a comfort issue, especially when personnel must inspect or manually intervene around the line.
Look beyond the main devulcanization chamber. Conveyors, discharge points, cooling sections, storage bins, and bagging stations may each contribute to the odor seen on the shop floor. Extraction hoods should be assessed under real production conditions, not only when the line is empty or running at low load. Airflow may need to be balanced with process containment; excessive open airflow around a transfer point can sometimes cool material unevenly or pull dust into areas where it does not belong.
This is one reason integrated equipment planning matters. JC INDUSTRY works across rubber and plastic machinery, environmental equipment, foundry systems, and digital tire mold technology. That broader equipment perspective is useful when a recycling line needs its process controls, material movement, maintenance access, and environmental measures to work together rather than operate as separate projects.
Cleaning Discipline Protects Process Stability
Residue buildup is often underestimated. Deposits on contact surfaces can retain degraded material and release odor during later heating cycles. They can also alter heat transfer, restrict movement, and introduce contamination into an otherwise stable batch. In lines that include curing-related equipment or metal processing support equipment, cleaning conditions should be defined as part of the operating procedure, not left to an informal end-of-shift task.
For example, a conveyor-belt curing press requires platen surfaces to be cleaned only after the heating platen temperature is below 60℃. The used_second hand Platen cleaning device is designed for this task and works with opening distances from 230 mm to 350 mm, using a 380V AC, three-phase, four-wire power supply. Its brush roller, remote control, and supplied spare parts address a practical maintenance need: keeping heating platens free of buildup without putting workers unnecessarily close to hot surfaces.
That example is not a substitute for reclaimed-rubber line cleaning plans, but the principle carries over. Maintenance equipment should be selected around actual access, temperature, lockout requirements, and contamination risks. A cleaning tool that cannot be safely used at the right time will not solve the underlying process problem.
What QC and Safety Teams Should Monitor Together
Quality and safety records are often kept separately, which makes it harder to see process drift. A more useful review compares production data with operator observations and workplace conditions. The following checks tend to reveal issues earlier than final-product inspection alone:
- Incoming feedstock identification, visible contamination, particle consistency, and storage duration.
- Actual temperature trends, not merely setpoints, across mixing, heating, discharge, and cooling stages.
- Motor load or torque changes that may indicate inconsistent feed, buildup, or altered material behavior.
- Odor changes reported by operators at specific points in the line and during specific shifts.
- Condition of seals, covers, extraction connections, filters, and housekeeping around transfer stations.
- Batch test results compared with the recorded operating window for that batch.
The goal is not to create excessive paperwork. It is to identify which variables move together. If odor increases whenever throughput rises, the issue may be insufficient residence-time control, overloaded extraction, or a feedstock change. If quality varies after cleaning intervals, residue accumulation or altered heat transfer may be part of the explanation.
A Better Machine Cannot Correct an Undefined Process
Equipment modernization can make reclaimed rubber production far more repeatable, particularly where intelligent control, enclosed handling, and process monitoring are integrated from the start. JC INDUSTRY has developed machinery across several industrial equipment categories and also operates a used machinery and equipment recycling center established in 2015. For plants considering refurbished equipment, the key question is not simply whether the machine can run; it is whether its control condition, safety functions, maintenance history, and integration requirements can support a defined quality window. JC INDUSTRY states that both new and used equipment are supplied with a 24-month warranty.
Still, odor reduction and batch uniformity come from disciplined operation as much as hardware. Define the acceptable feedstock, establish limits for critical processing conditions, inspect containment and cleanliness routinely, and investigate odor changes before they become a rejection trend. When those basics are in place, a reclaimed rubber machine becomes a practical control tool rather than another source of variability.